What is Vacuum Pump oil?
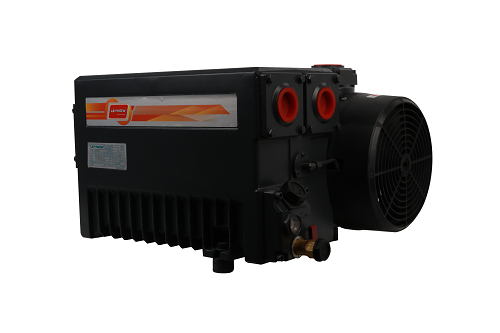
Vacuum Pump Oil is the dedicated lubricant (working medium) for oil-sealed mechanical Vacuum pumps, not ordinary engine oil, hydraulic oil or gear oil. Its core characteristic is extremely low saturated vapour pressure.
1. Three core functions (the biggest difference from ordinary lubricants)
Sealing: fills the clearances between vanes and pump body, blocking gas leakage and directly determining how high a vacuum can be reached;
Lubrication: lubricates the internal rotor and vane friction pairs;
Cooling and dust carrying: removes compression heat and absorbs dust and moisture.
Key indicator: extremely low saturated vapour pressure
Ordinary engine oil contains many light fractions that vaporise easily under negative pressure, directly causing poor vacuum and oil backstreaming that contaminates workpieces. It must never be used instead of vacuum pump oil.
2. Two main categories
1) Mineral vacuum pump oil (most common, cost-effective)
Deeply refined mineral base oil from crude plus antioxidant and anti-emulsification additives
Common grades: 46, 68, 100 (V100); Leno VG100 and Huifeng HFV100 belong to this category
Applications: standard Rotary Vane Vacuum Pumps, Packaging machines, air conditioning evacuation pumps, general industrial air evacuation
Drawbacks: moderate high-temperature resistance, prone to oxidation and coking under prolonged high temperature
2) Synthetic vacuum pump oil (high-end duty)
Chemically synthesised base oils, subdivided into:
PAO synthetic hydrocarbon oil: good heat resistance, long life;
Ester oils: thermally stable, suited to continuous high-temperature duty;
Perfluoropolyether (PFPE) oil: resistant to strong corrosion and oxidising agents (chemical, semiconductor), very expensive;
Silicone oil: mostly used in diffusion pumps and ultra-high vacuum equipment.
Applications: coating, Freeze Drying, pumping corrosive gases in chemical plants, equipment running continuously at high temperature for 24 hours.
3. Common misconceptions
Never substitute engine oil, Air Compressor oil or hydraulic oil.
Ordinary oils have high vapour pressure, cannot reach rated vacuum and easily form carbon deposits that damage vanes;
Do not mix different types of vacuum pump oil at will (mineral oil is not synthetic oil);
Most common for rotary vane pumps: grade 100 vacuum pump oil (HFV100/VG100); small direct-coupled pumps commonly use 46 or 68.
4. Quick selection guide
Small Vacuum Pumps for air conditioning repair: grade 46 or 68 vacuum pump oil
General industrial rotary vane vacuum pumps (Jung, Leno and other domestic pumps): grade 100 mineral vacuum pump oil
High temperature or continuous operation without shutdown: synthetic vacuum pump oil
Pumping corrosive solvents and strong acid gases: PFPE perfluoro oil