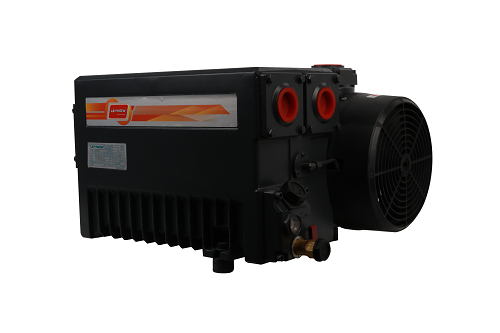
The oil-sealed Rotary Vane Vacuum Pump is core general equipment in Vacuum Packaging, Vacuum coating, fine chemicals and electronics processing, yet Vacuum Pump oil, the lifeblood of its operation, has long been neglected by many manufacturers. Many users confuse Vacuum Pump Oil with ordinary lubricants, resulting in insufficient vacuum, premature equipment wear and production line downtime. As a brand deeply engaged in vacuum equipment, Leno rotary vane vacuum pumps, drawing on a large number of industrial field cases, remind the industry that vacuum pump oil is a dedicated medium and must never be replaced at will with engine or hydraulic oil; correct oil selection is the basic precondition for unleashing vacuum pump performance.
The core indicator that distinguishes vacuum pump oil from conventional lubricants is its extremely low saturated vapour pressure, together with its three key functions of sealing, lubrication and Cooling. During rotary vane pump operation the oil forms a film that fills the tiny clearances between vanes and pump body, blocking gas backflow and maintaining a stable ultimate vacuum; it also continuously lubricates the high-speed vanes and rotor structure, carries away compression heat, and absorbs dust and condensed moisture. Leno rotary vane vacuum pumps use a precision vane structure with tight clearance control in the pump body, imposing strict requirements on oil film stability. Practice shows that when the oil performance is inadequate, even with the mechanical performance of the Leno pump intact, vacuum will still decline and exhaust oil carryover will contaminate workpieces, directly affecting finished product yield.
The mainstream vacuum pump oils on the market fall into two categories, mineral and synthetic, with markedly different applicable duties. Mineral vacuum pump oil is widely used for its cost-effectiveness, with common grades 46, 68 and 100, suited to conventional intermittent production. Synthetic vacuum pump oils include synthetic hydrocarbons, esters and perfluoropolyethers, offering stronger high-temperature resistance and chemical corrosion resistance, suited to 24-hour continuous operation and duty pumping corrosive solvents. Leno rotary vane vacuum pumps cover small portable pumps and industrial single-stage rotary vane pumps in multiple series, with clear oil guidance for different duties: grade 46 or 68 vacuum pump oil for small air conditioning repair models; grade 100 mineral vacuum pump oil for food packaging and general industrial production lines; and synthetic vacuum pump oil for chemical, coating and other high-temperature continuous duties, giving full play to stable pumping performance.
Several typical oil misconceptions are common in the industry and are frequently encountered by Leno's after-sales team during Maintenance service. Some enterprises substitute engine oil or Air Compressor lubricant for vacuum pump oil to save cost. Such oils contain many light components that vaporise easily under negative pressure; they not only fail to reach the target vacuum but also continuously form carbon deposits that seize the vanes. Mineral and synthetic oils must never be mixed at will either, since mixing disrupts the additive system and accelerates oil failure. Leno rotary vane vacuum pumps are designed with long-term maintenance in mind and come with clear oil change interval specifications; using the correct vacuum pump oil effectively extends the life of vanes and bearings and greatly reduces spare parts spending.
As intelligent manufacturing upgrades, industries demand ever greater vacuum process stability, and refined Vacuum System maintenance has become an industry trend. Equipment hardware quality and consumables complement each other: only a high-quality rotary vane vacuum pump combined with compliant dedicated vacuum pump oil can maintain design pumping speed and ultimate vacuum over the long term. In future, Leno will continue to draw on extensive industrial application data from rotary vane vacuum pumps to popularise vacuum equipment maintenance knowledge, and to provide customers in food, pharmaceutical, electronics and new materials industries with integrated vacuum solutions covering equipment selection, oil matching and full-lifecycle maintenance, helping enterprises achieve efficient, low-cost continuous production.